Bucket Elevator Manufacturing | Ommix Vertical Conveying Solutions
Ommix Bucket Elevators: Safe and Efficient Vertical Handling Solutions for Your Materials
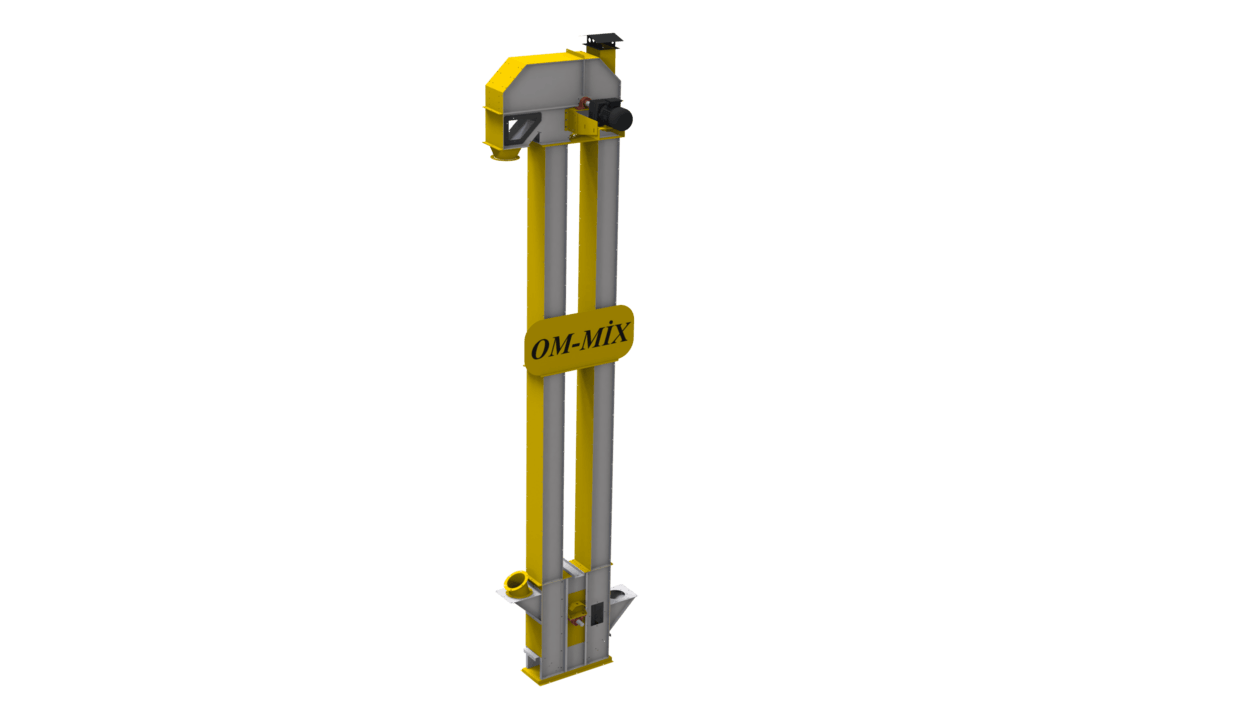
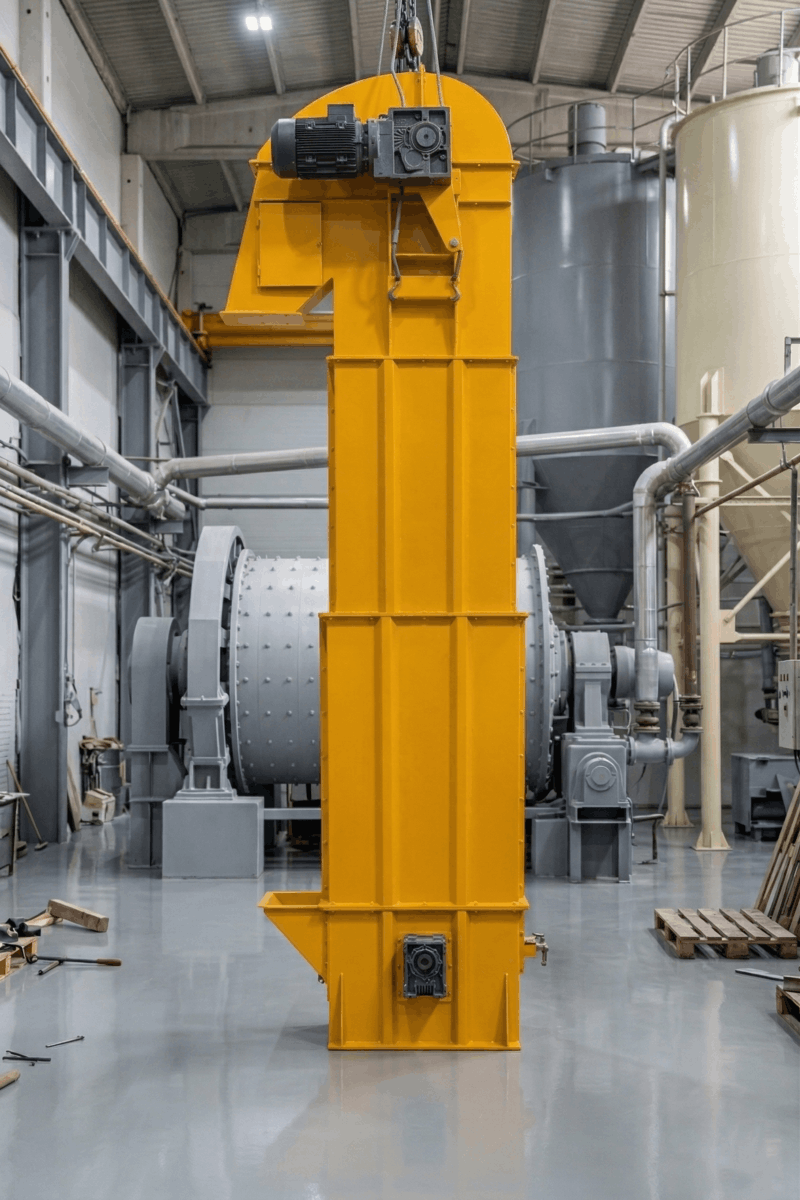
In industrial facilities, the vertical transport of powders, granules, and other bulk materials from one level to another is one of the most critical elements of operational efficiency. At Ommix Makine, we manufacture bucket elevators specifically designed to meet the needs in this area . Thanks to their high-performance and durable construction, we guarantee the safe and efficient transport of materials at every stage of your production line.
Features of Ommix Bucket Elevator Systems
- The Ideal Solution for Powder and Granular Materials: Our bucket elevators are specifically designed for the vertical conveyance of powder and granular materials such as cement, sand, grain, flour, feed, spices, and chemical granules. We offer different bucket and belt options depending on the material's composition to ensure maximum efficiency.
- Flexibility in Capacity and Size: We understand that every project has its own unique requirements. Therefore, we manufacture bucket elevators in various sizes and lengths to suit your facility's installation area and lifting capacity . We work with our engineering team to provide you with the most suitable solution for your vertical conveying needs.
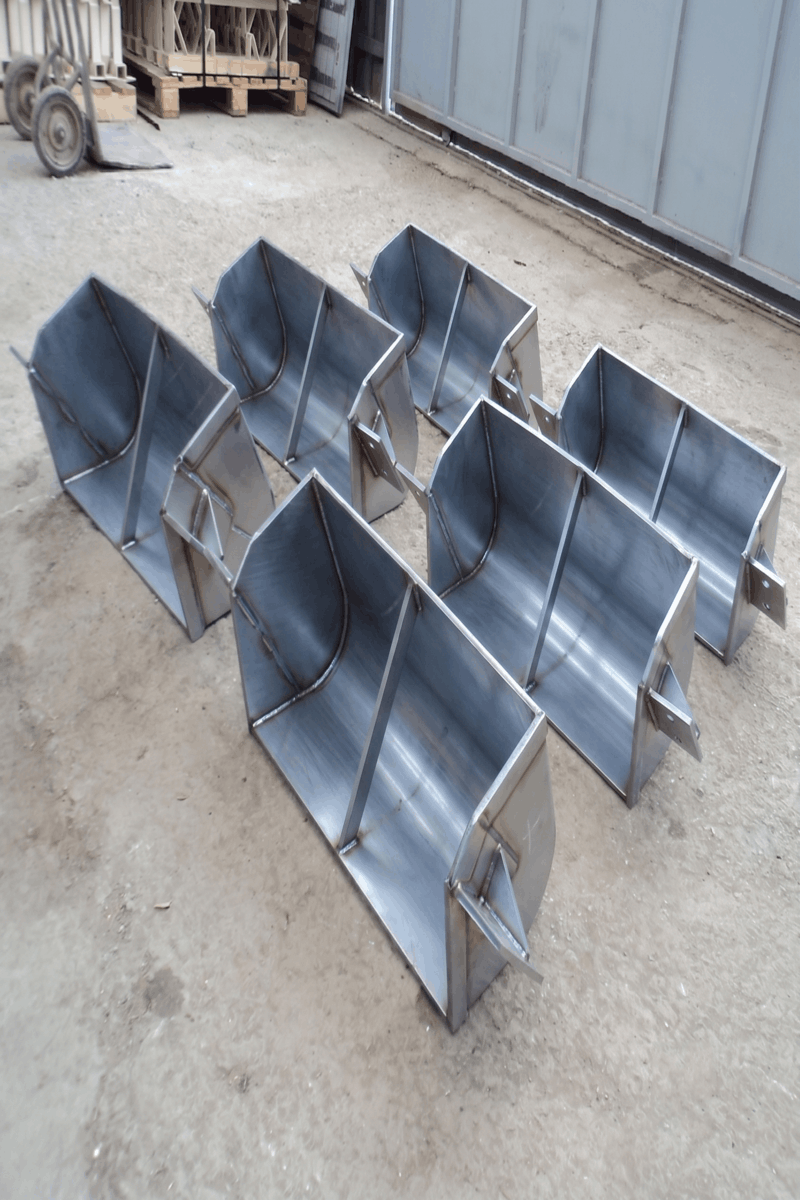
- Superior Durability and Long-Lasting Construction: The body structure of our bucket elevators is manufactured from materials resistant to wear and corrosion (carbon steel or stainless steel). With a robust chain or belt system and impact-resistant buckets, they offer long-lasting and trouble-free performance even under the most demanding working conditions.
- Safety and Ease of Maintenance: Our systems are designed in accordance with occupational safety standards. Thanks to special covers and access points that facilitate maintenance and cleaning , operational interruptions are minimized and personnel safety is maximized.
- Energy Efficiency: Ommix elevators minimize energy consumption with optimized motor and drive systems while offering high lifting capacity. This results in significant savings on operating costs.
Areas of Application
- Cement and Building Materials Industry: Transportation of cement, sand, gypsum, and lime.
- Food and Agriculture Industry: Transportation of grains, flour, feed, and legumes.
- Plastics and Chemical Industry: Vertical conveying of granular and powdered chemicals.
- Mining: The transportation of ores and minerals.
Frequently Asked Questions
For which materials are bucket elevators ideal?
Bucket elevators are used especially for the vertical conveying of bulk materials, particularly powders and granules.
In what capacities are Ommix bucket elevators manufactured?
We manufacture custom-made products to meet the specific needs of each project, therefore offering flexible solutions in terms of capacity and size.
Is bucket elevator maintenance difficult?
No. Our products are equipped with easily accessible maintenance covers, allowing maintenance and repair processes to be carried out quickly and easily.
How do bucket elevators work?
Our elevators transport material vertically from the material feeding point via hoppers to the desired height and discharge it at the discharge point. Because this process takes place within a completely closed system, material loss and dust dispersion are prevented.